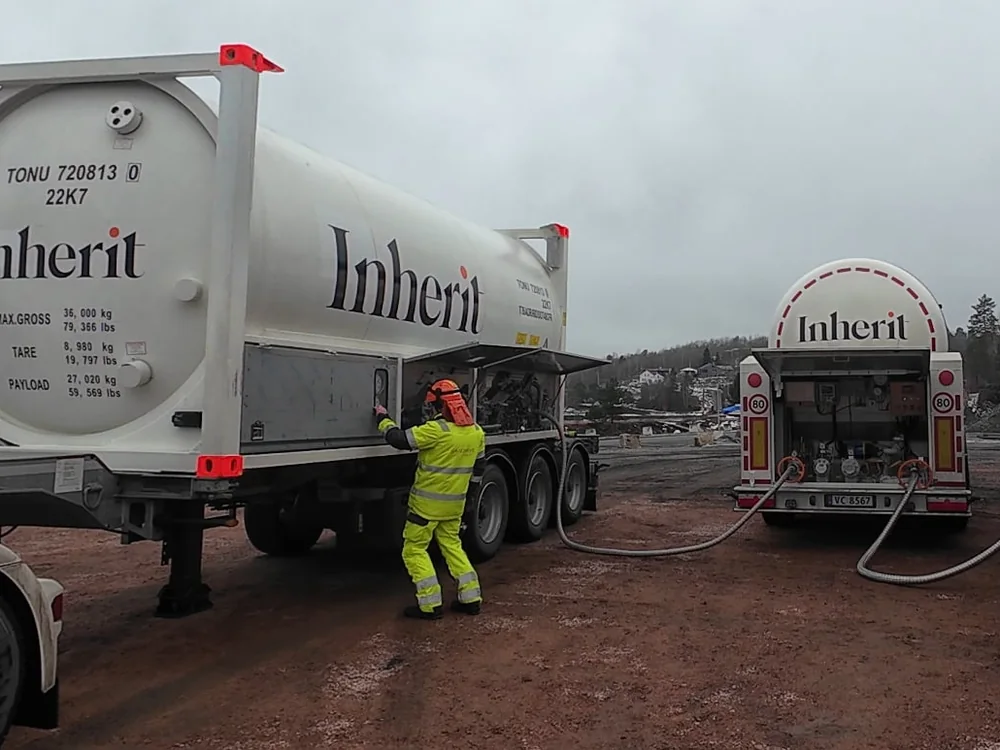
Cryogenic ISO tank containers are designed to withstand a certain service temperature; these are always significantly below the ambient temperature. Therefore, the system must be cooled down to the temperature of the load prior to transfer. Foregoing on cooldown may result in material stress and a thermal shock caused by an over-rapid cooling of the system, resulting in the steel of the inner shell becoming brittle and/or fractures. The other key reason for performing a cooldown is that, if a cryogenic liquid is introduced directly into a “warm” (or ambient) tank, the cryogenic gas will immediately turn into vapour. Cryogenic gases have a liquid to gas expansion ratio of 1 to 600, resulting in rapid, potentially dangerous pressure build up inside the tank (“flash gas”).
Cooldown is required prior to loading all cryogenic liquefied gases. The procedure consists of gently introducing cold vapour and liquid to the tanks, for instance through spraying cold nitrogen through the spray pipes of the tank.
Cooldown is the pre-cooling of cryogenic tank containers and lines, required before loading cryogenic flammable gases. Cryogenic ISO tank container cooldown is carried out by spraying nitrogen through the spray nozzles of each tank. The cooldown operation from an ambient temperature to a planned temperature is called ‘initial cooldown’ and is to be differentiated from an ordinary cooldown operation carried out during transit. Before a flammable gas can be introduced into a cryogenic tank container, the tanks have to be cooled down to a temperature close to that of the gas which is to be loaded. The reasons for this are as follows:

If a cryogenic gas is introduced directly into warm tanks, the cryogenic gas will almost immediately turn into vapour. LNG for example has a liquid to gas expansion ratio of 1:600. Therefore, to enable the liquid to be loaded into the tank at a reasonable loading rate, large compressors would be required to remove the vapour generated in the process. By reducing the cargo tank temperature, the amount of heat that is available to transfer into and heat the LNG is minimized. Consequently the amount of vapour generated can be maintained within reasonable limits.
Bofort’s cryogenic ISO tank containers are constructed of stainless steel which retains its flexibility and strength characteristics over the temperature range being considered (-196 °C to +50 °C). However, problems could occur if the material is subjected to very local and rapid cooling such as when a small droplet of cryogenic gas comes into contact with a warm tank wall. Because of the transfer of the heat from the wall into the liquid, the temperature at the particular point will decrease rapidly causing large thermal stresses to arise between the point and the surrounding material. This could lead to stress cracking (a so-called cold spot).

The pipe-work with the tank is constructed of stainless steel tubes. If subjected to rapid cooling, thermal stress within the material can be excessive, leading to the material cracking. All three reasons are of equal importance as each, if not carefully controlled, can have a significant impact on the tank structure and overall safety of the tank.
After the cargo system has been gassed up the headers and tanks must be cooled down before loading can commence. The rate of cooldown is limited for two reasons: the vapour generated must remain within the capacity of the compressors, and the tank pressure must stay safely below the set pressure of the safety valves. Nitrogen is supplied from the terminal or other supply to the cooldown line and from there directly to the spray header. The various spray valves are operated in order to produce a temperature profile in line with, but not exceeding the manufacturers’ instructions. Some tanks may require a minimum temperature before bulk loading may commence; this temperature is to be strictly adhered to.